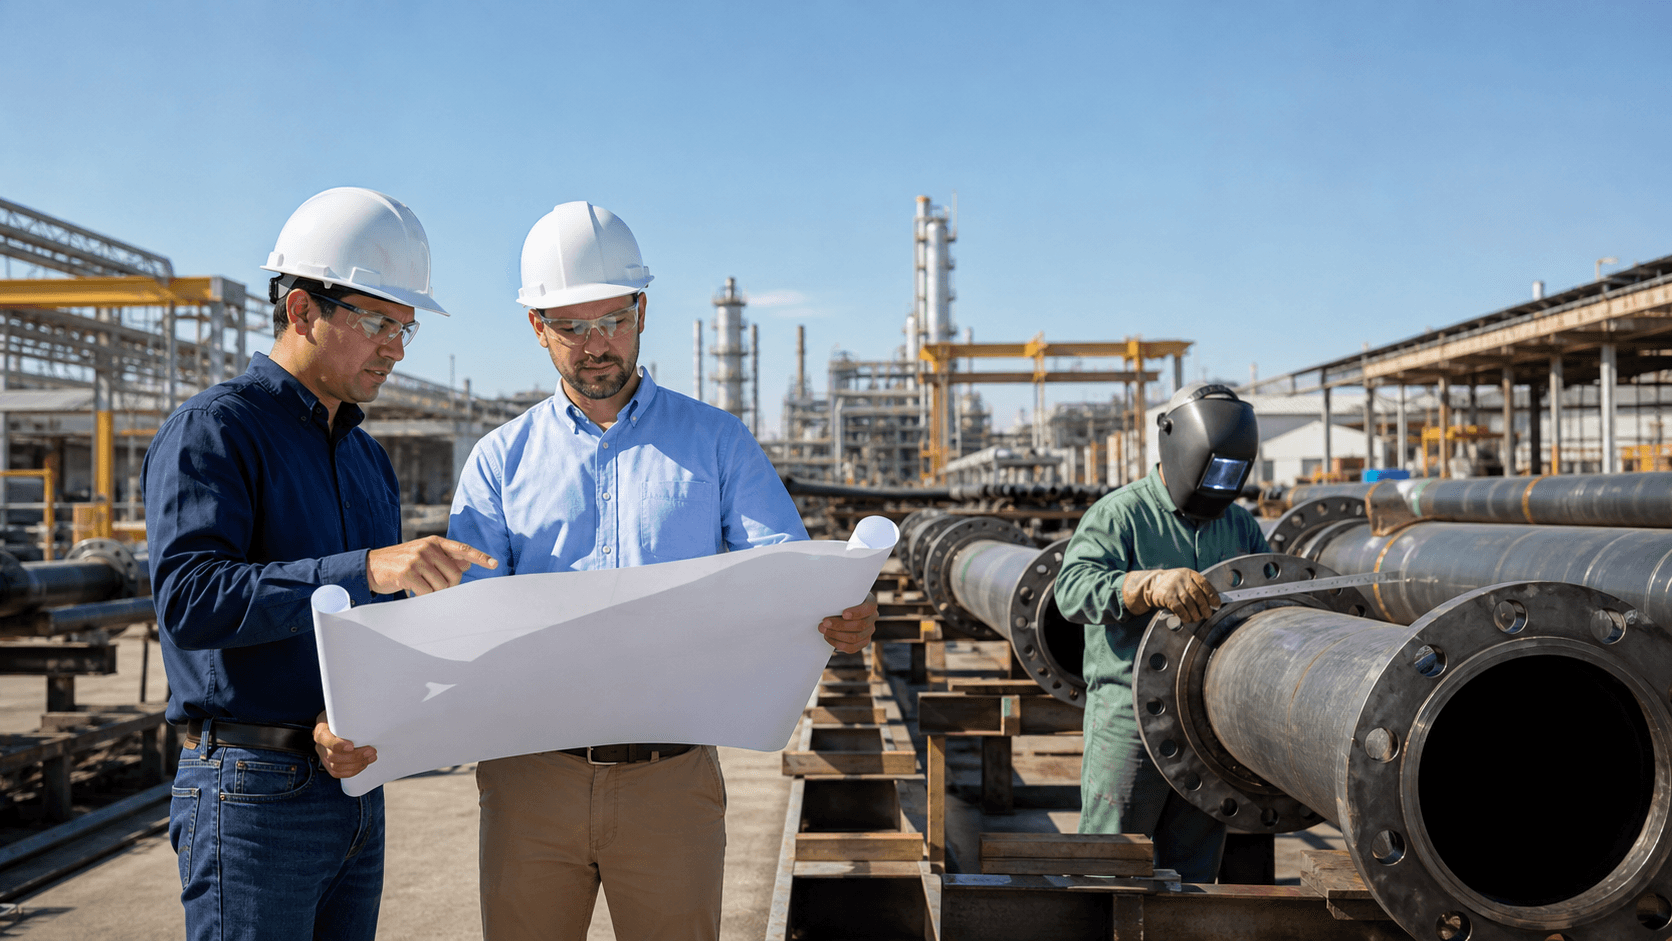
Pipe spooling RFIs can make or break your fall work in Houston facilities. When the questions are vague, vendors guess, inspectors push back, and your crew waits on drawings, weld maps, or missing MTRs instead of installing pipe. Clear, tight RFIs give you real dates, clean traceability, and test packs that pass without drama.
In this guide, we share plain, copy‑paste RFI questions you can send to pipe spooling vendors. We focus on four big risk areas: lead times, spool tracking and heat numbers, test packs, and turnover documentation. Use these questions to keep your schedule moving and your documentation ready for owner and third‑party review.
Stop Losing Days on Pipe Spooling RFIs in Houston
During fall outages and pre‑holiday reliability projects, every day on the schedule matters. A single unclear RFI about pipe spooling can stall shop work, NDE, coating, or delivery across the Houston area.
Vague questions often lead to:
- Guesswork on lead times that slips into the outage window
- Spool IDs that do not match your P&IDs or iso drawings
- Heat numbers that are hard to trace in the field
- Test packs that inspectors reject or send back for edits
Instead of asking "Can you handle this scope?" you need specific questions on how and when the work will be done, how it will be tracked, and how it will be documented. The rest of this article breaks those questions down by topic so you can plug them straight into your RFIs.
Nail Pipe Spooling Lead Times Before Turnaround Season
First, you need real dates, not guesses. Ask vendors to break out their schedule so you can line it up with your outage and MOC plan.
Key RFI questions on lead time pieces:
- "Please provide separate durations for material procurement, shop detailing, fabrication, NDE, coating, and delivery to our Houston facility for this scope."
- "For each pipe size, schedule, and alloy listed, give best‑case, typical, and worst‑case lead times using your current AWS and ASME weld procedures."
- "List all constraints that can move dates, including QC hold points, owner inspection windows, holidays, and any site access limits during the outage."
You also want to know if they can surge when your design team issues late RFIs or revised isos.
Ask about capacity and surge support like this:
- "How many code‑compliant spools per week can you realistically produce for this diameter and schedule mix?"
- "Do you have mobile welders available for field changes or extra tie‑ins without slipping overall schedule milestones?"
- "Share examples of how you have supported rush pipe spooling for Houston facilities during previous fall projects."
Then tie those answers into your own schedule:
- "Map your fabrication milestones to our shutdown and commissioning dates and identify any conflicts with our critical path activities."
- "Provide a contingency plan for priority spools, such as tie‑ins and safety‑critical lines, if we issue late design changes."
- "Explain how your lead times change if we phase work into pre‑shutdown prefabs and outage tie‑ins."
Get Spool Tracking and Heat Numbers Right the First Time
Numbering mix‑ups cost time in the field. Fix that upfront in the RFI.
Start with their tracking structure:
- "How do you assign spool IDs, weld numbers, and heat numbers, and how do those link back to P&IDs and isometrics?"
- "Provide a sample spool map and ID schema in PDF or spreadsheet format for our review before we release bulk work."
- "Can you follow our existing plant spool numbering and tag hierarchy as shown in the attached standards?"
Heat number traceability is just as important:
- "How are heat numbers physically marked on spools and components, and how is that information captured digitally?"
- "Send sample MTRs that show how each heat number is tied to specific welds and spool IDs."
- "Describe your process for maintaining traceability when cutting stock lengths or substituting material because of supply limits."
Finally, make sure the data will fit your QA system:
- "What file formats can you provide for tracking data, such as Excel, CSV, or exports from your QC software?"
- "Can spool IDs, weld maps, and heat numbers be delivered in a way that is searchable by line number and service description?"
- "Confirm that any mobile welding or field‑fit spools will follow the same tracking and heat number protocol as shop spools."
Specify Test Packs That Pass Houston Inspections
Incomplete or hard‑to‑follow test packs slow down walkdowns and sign‑offs. Set expectations clearly in the RFI so there are no surprises.
Start with code basis and inspection scope:
- "Which AWS and ASME code sections will you use to qualify procedures and welders for these services, including process, hydrocarbon, and steam lines?"
- "Provide a matrix of NDE types, such as RT, UT, MT, and PT, by line class or criticality, aligned with our standards."
- "Confirm pressure test requirements, including hydro or pneumatic tests, test pressures, hold durations, and any needs for late‑season testing conditions."
Then ask for example‑ready test packs:
- "Submit a sample test pack from a recent Houston project that includes P&IDs, isometrics, weld maps, NDE reports, MTRs, and test certificates."
- "Explain how each test pack will link spools, welds, and line numbers to specific test results and acceptance criteria."
- "Describe how open punch items, failed welds, and retests will be logged, tracked, and closed inside the test pack."
You also need alignment with owners and authorities:
- "How early can you provide test pack templates for owner and third‑party inspector review before testing?"
- "Can your team join pre‑test coordination meetings to confirm documentation, witnessing, and sign‑off procedures?"
- "What is your process to update test packs when RFIs lead to design changes, new tie‑in points, or revised testing sequences?"
Demand Turnover Documentation That Actually Works on Site
Turnover is where missing pieces show up. Define "done" in your RFI so your team is not chasing stray weld logs during startup.
First, list what you expect at mechanical completion:
- "List every document and record that will be provided at construction turnover, including redlines, weld logs, MTRs, NDE summaries, test certificates, and as‑built isos."
- "Clarify the difference between your construction turnover package to us and the final turnover set for operations."
- "Explain how emergency repair spools and field‑added work will be merged into the main turnover package."
Ask for format and structure that people can use in the field:
- "Provide a proposed index template that is organized by unit, system, line number, and spool ID."
- "Confirm that you can provide both searchable digital copies and field‑ready hard copies for inspectors and operators."
- "Share your file naming standards so our team can quickly find documentation for any given spool or weld."
Then tie documentation to long‑term reliability:
- "How will your documentation support future MOC, RBI, and PM planning, including weld history and any alloy changes?"
- "Confirm that code stamps, welder qualifications, and procedure records will be clearly traceable for future audits."
- "Describe how outstanding RFIs, NCRs, and punch items will be closed out in the final turnover package, with responsible parties and dates."
Turn Better RFIs Into Faster, Safer Pipe Spooling Work
Clear RFIs do more than move paperwork. They protect outage dates, reduce rework in the field, and give inspectors what they need to sign off without delays. In a busy Houston facility, that can be the difference between a clean restart and a rushed scramble.
By asking specific questions on lead times, pipe spooling capacity, spool tracking, heat numbers, test packs, and turnover documentation, you set expectations that everyone can follow. As a certified industrial and commercial welding contractor based here in Texas, we see how much smoother projects run when these points are ironed out early, for both shop fabrication and mobile welding work across major markets.
Get Started With Your Project Today
If you are planning a complex industrial project, we can help you streamline fabrication with precise, well-coordinated pipe spooling solutions. At Weldit, we work closely with your team to align our shop drawings, materials, and weld quality with your project schedule and specifications. Share your requirements with us through our contact page so we can provide a clear path, from initial quote through final delivery.